High Performance Fabrics from yarn wholesale manufacturers
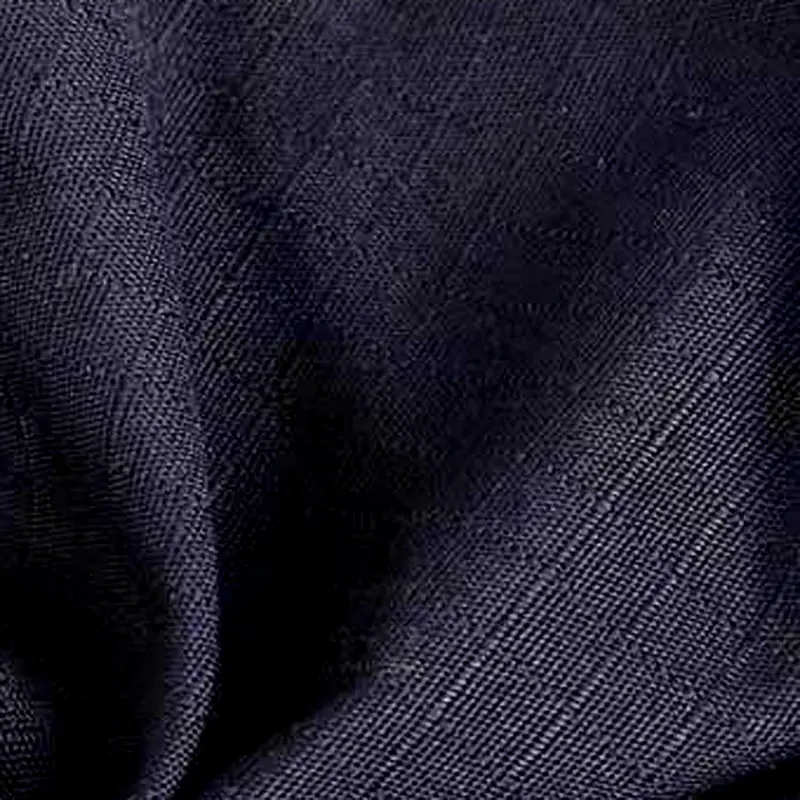
When sourcing high-performance textiles for outdoor and specialized apparel, the balance between breathability and environmental protection is critical. The cotton nylon plain dyed coating fabric provides a strategic blend of 70% natural cotton for comfort and 30% synthetic nylon for structural integrity and durability. This specific composition is engineered to meet the rigorous demands of protective outerwear, where windproof performance and moisture resistance are non-negotiable requirements for the wearer's safety and comfort.
For procurement specialists and garment designers, selecting a material that combines a smooth aesthetic with functional reverse-side coating is essential for producing high-end raincoats, ski suits, and mountaineering gear. By integrating advanced coating technology, this fabric transitions from a standard textile to a functional barrier capable of repelling rain and blocking wind, making it a primary choice for those seeking reliable materials from experienced yarn wholesale manufacturers.

Technical Composition and the Synergy of Cotton and Nylon Blends
The efficacy of this coating fabric lies in its precise 70/30 ratio. Cotton provides the necessary softness and skin-friendliness, ensuring that the garment remains breathable and comfortable during prolonged wear. Meanwhile, the 30% nylon component introduces essential tensile strength, abrasion resistance, and a degree of natural elasticity that prevents the fabric from tearing under the stress of outdoor activities like skiing or climbing.
The plain dyed process ensures color consistency across large production batches, which is vital for brand uniformity in commercial clothing lines. The most critical technical feature, however, is the smooth fabric color coating applied to the reverse side. This layer acts as a hydrophobic barrier, significantly enhancing the windproof capabilities and providing the rainproof characteristics required for extreme weather conditions.
- Material Ratio: 70% Cotton / 30% Nylon for optimal comfort and strength.
- Coating Logic: Reverse-side smooth coating for wind and water resistance.
- Surface Finish: Plain dyed for high color stability and professional appearance.

Application Scenarios for Advanced Waterproof and Breathable Outerwear
The versatility of the cotton nylon plain dyed coating fabric makes it ideal for a wide range of specialized apparel. In the realm of alpine sports, it is frequently used for ski suits that require advanced waterproof and breathable functions. The coating ensures that external moisture and wind are blocked, while the cotton-rich face allows for a level of vapor transmission that prevents the wearer from overheating.
Beyond sports, this material is highly effective for professional mountaineering suits and windcoats. In these scenarios, the fabric must withstand constant friction against rocks and equipment, a task handled by the nylon reinforcement. Its rainproof characteristics ensure that light to medium precipitation does not penetrate the garment, maintaining the core body temperature in unpredictable environments.
Furthermore, the fabric is suitable for high-quality raincoats intended for urban and semi-rural use, where a more natural look and feel (provided by the cotton) is preferred over the plastic-like appearance of 100% synthetic waterproofs.
Manufacturing Excellence and Quality Assurance in Functional Textiles
Producing functional coated fabrics requires a sophisticated manufacturing infrastructure. The process involves not only precision weaving but also the application of a uniform coating that does not compromise the fabric's drape or flexibility. Quality control focuses on the adhesion of the coating to the base fabric, ensuring it does not peel or crack over time or after repeated folding.
Consistency in dyeing is another critical factor. Using advanced dyeing technology ensures that the "plain dyed" finish is deep and uniform, avoiding streaks or patches. For global buyers, certifications such as ISO9001 and Oeko-Tex Standard 100 provide the necessary assurance that the chemical processes used in coating and dyeing are safe for the end-user and the environment.
The ability to scale production while maintaining these tight tolerances is what separates leading manufacturers from small-scale workshops. Industrial-grade looms and automated coating lines are essential to ensure that every meter of fabric provides the same level of windproof and waterproof protection.
Technical Comparison of Coated Fabric Performance
| Performance Metric | Uncoated Cotton/Nylon | Coated Cotton/Nylon | 100% Synthetic Coated |
|---|---|---|---|
| Windproof Level | Low to Medium | High | Very High |
| Breathability | Very High | Medium-High | Low to Medium |
| Skin Comfort | Excellent | Good | Moderate |
| Water Resistance | Absorbent | Rainproof | Waterproof |
| Durability | Medium | High | Very High |
Procurement Considerations for Wholesale Functional Fabrics
When engaging with yarn wholesale manufacturers, procurement managers should evaluate the specific type of coating used. Not all coatings are created equal; some offer better breathability, while others prioritize absolute water blockage. It is essential to request technical data sheets that specify the hydrostatic head (water column) and the moisture vapor transmission rate (MVTR).
Another key consideration is the compatibility of the fabric with various sewing techniques. Coated fabrics can sometimes be prone to needle holes becoming leak points, so the quality of the base weave and the flexibility of the coating are paramount. Buyers should also consider the shrinkage rates of the cotton component to ensure that the final garment dimensions remain stable after the manufacturing process.
Finally, sustainability is becoming a primary driver in textile procurement. Inquiring about the organic nature of the cotton or the use of recycled nylon can help brands meet their ESG (Environmental, Social, and Governance) goals without sacrificing the functional performance of the outerwear.
Future Trends in Hybrid Coated Textiles and Protective Gear
The industry is moving toward "smart" coatings that can adapt to environmental changes. Future iterations of cotton-nylon blends may include coatings that offer antimicrobial properties or UV protection, further expanding the application of these fabrics into medical protective wear or extreme sun-exposure gear.
We are also seeing a shift toward bio-based coatings to replace traditional synthetic polymers. This transition aims to maintain the windproof and rainproof characteristics of the current coated fabrics while significantly reducing the carbon footprint of the production process. This evolution ensures that high-performance gear remains viable in a more environmentally conscious market.
As consumer demand for "athleisure" grows, the blending of professional-grade functional fabrics with everyday comfort will continue. The cotton nylon plain dyed coating fabric is a prime example of this trend, offering the technical protection of a ski suit with the tactile comfort of a casual garment.
Frequently Asked Questions About Coated Functional Fabrics
What makes the 70% cotton and 30% nylon blend superior for outerwear?
This blend combines the natural breathability and comfort of cotton with the strength and durability of nylon. The result is a fabric that feels comfortable against the skin while resisting the wear and tear typical of outdoor environments.
Is the reverse-side coating effective against heavy rain?
The coating provides excellent rainproof and windproof characteristics, making it suitable for raincoats and windcoats. While highly resistant, its primary strength is blocking wind and repelling water in typical outdoor conditions.
Can this fabric be used for high-altitude mountaineering?
Yes, it is specifically designed for mountaineering suits and ski suits due to its ability to block wind and provide necessary water resistance while remaining breathable.
How does the "plain dyed" process affect the fabric?
Plain dyeing provides a consistent, solid color across the entire textile. This ensures a professional look for commercial apparel and prevents color variance between different production lots.
Does the coating affect the breathability of the cotton?
The coating is engineered to provide a balance. While it creates a barrier against wind and water, the cotton-rich composition helps maintain a level of breathability superior to 100% synthetic waterproof fabrics.
What should I check when sourcing this fabric from a manufacturer?
Buyers should verify the coating adhesion quality, the color fastness of the plain dye, and ensure the manufacturer holds certifications like ISO9001 or Oeko-Tex for quality and safety.
Industry Technical References
- Textile World - Functional Fabric Trends
- ISO Quality Management Standards for Textiles
- Oeko-Tex Standard 100 Certification Guidelines
- Cotton Incorporated - Technical Material Properties
Choosing the right functional fabric requires a deep understanding of material synergy and coating technology. Whether you are designing for professional athletes or urban commuters, the cotton nylon plain dyed coating fabric offers a reliable solution for wind and water protection.
Explore Our Functional Textile Portfolio
 Skin-friendly
 Versatile
 Durable
 Assured

